| Consideration | What it affects | Direction |
|---|---|---|
| High energy from rotation | How fast material is removed | Shorten the cycle rather than extend it |
| Barrel shape | How the load tumbles inside | Hexagonal barrels change the contact pattern |
| Edge condition | How much the part may lose | Check edges on a sample before a full run |
| Load per barrel | Consistency between barrels | Load each barrel the same way |
| Media selection | Which surfaces are reached | Size from the smallest feature |
| Component wear | Maintenance interval | Inspect liners and drives at intervals |
Directions to test on a representative sample, not validated results for a specific component.
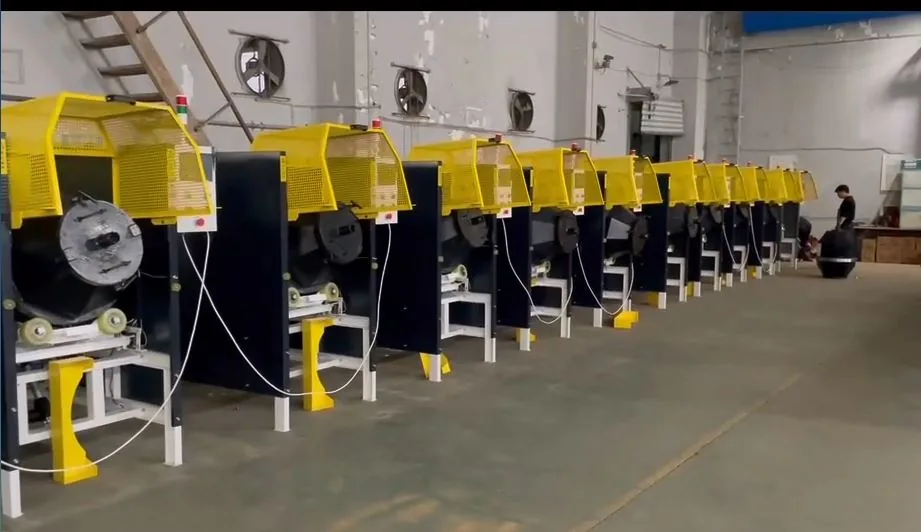
A hexagonal barrel is not a round barrel with corners. The flat faces change the way the load moves inside the drum: instead of the charge sliding down a smooth wall, it is lifted by a flat face and falls in a defined pattern. That produces a more predictable tumbling action and a different distribution of contact across the load.
The practical effect is usually a faster and more uniform action than a round drum of the same size, because the charge is turned over more consistently. The trade-off is that the action is also more energetic. Parts that a round drum would treat gently can be marked or rounded in a hexagonal drum at the same load and cycle, which is why the process is normally dialled in on a sample rather than transferred directly from a round-drum result.
Three parameters decide what a hexagonal barrel does to a part. Load per barrel comes first, because each barrel has to be loaded so the charge can turn over. An uneven load between barrels changes the action in each one, and the result is a batch that varies from barrel to barrel rather than a batch that is uniformly over- or under-worked.
Media selection comes second. The size has to suit the smallest feature that must be reached, and the grade has to suit the surface the part is allowed to lose. With a high-energy barrel, the consequences of choosing too coarse a media appear sooner than they would in a slower process.
Cycle time comes last, and it should be short. The advantage of a high-speed barrel is that it reaches a result quickly; lengthening the cycle past that point removes material without improving the surface. Where a longer or gentler finish is needed, the usual approach is to follow the barrel with a lower-energy finishing stage.
Email : info@surface-polish.com


 IPv6 network supported



 +86-592-2381506
