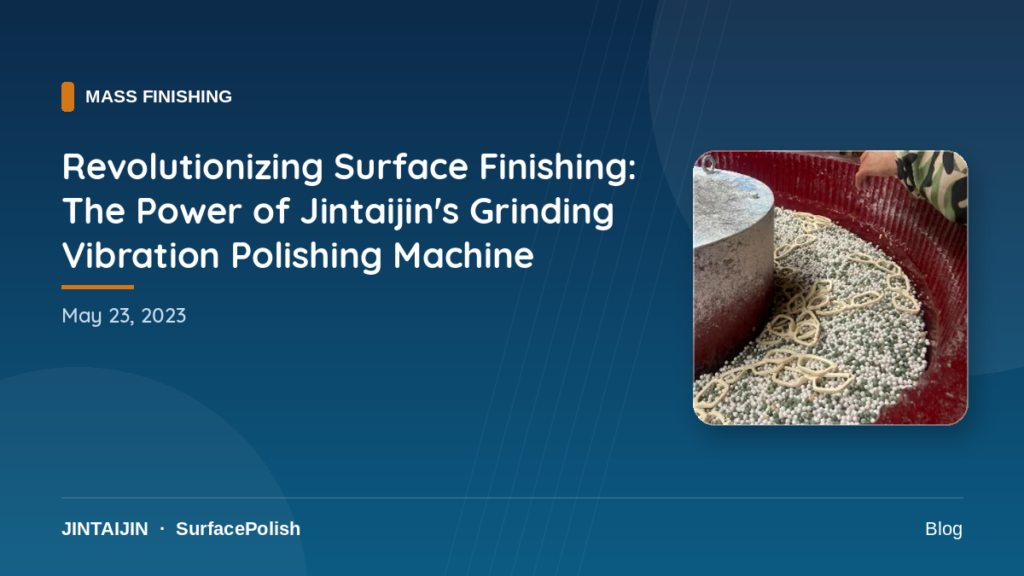
In a rotating barrel, the load moves because gravity moves it: the drum lifts the charge and it falls. That gives a gentle but relatively slow action, and it means the media follows a predictable path. A vibrating machine replaces gravity with vibration, and that change has two consequences worth understanding.
The first is speed. Because the media is in constant motion rather than being lifted and dropped once per revolution, the part sees far more contacts per unit of time. The same amount of surface work happens in a shorter cycle. The second is reach. Vibration drives media into recesses and around internal forms in a way that a falling charge does not, which is why vibrating machines can work features that a barrel leaves untouched.
Neither advantage is free. The greater energy that produces speed also removes material faster and rounds edges sooner. On a part where the edge is functional, a cycle that is efficient for one component can be destructive for another with the same nominal finish requirement.
The useful order of decisions is: what feature must be reached, what the part may lose, and how much throughput is needed. The first decides whether the media can physically enter the feature. The second decides how much energy the process can apply. The third decides between a vibratory process and a higher-energy one.
Vibrating machines come in bowl and tub forms, and the shape matters for the part rather than for the finish. A bowl circulates the load uniformly and suits smaller parts in volume; a tub gives the charge a longer path, which suits long, heavy or awkwardly shaped components that do not circulate well in a round chamber. The finish these two produce is set by the media and the cycle, not by the chamber shape.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
