


This guide is based on common surface finishing scenarios observed across production facilities. The recommendations here apply to typical metal and plastic parts processed in vibratory finishing, barrel tumbling, disc finishing, and related mass finishing equipment. Specific results vary by material, part geometry, equipment condition, and operator technique.
Key Process Variables to Consider
Every finishing process has five primary variables that control the outcome. Understanding how they interact is the foundation of consistent quality:
- Media type, size, and condition: determines the cutting or polishing action on the part surface.
- Compound chemistry and concentration: controls cutting speed, surface finish, cleaning, and corrosion protection.
- Machine motion (speed, amplitude, vibration pattern): affects how media contacts the part and how energy is transferred.
- Water quality and flow (for wet processes): carries compound, removes debris, and affects chemical reaction rates.
- Part loading density and separation: determines whether parts contact each other and how uniformly media reaches all surfaces.
Common Mistakes to Avoid
- Changing multiple variables at once. When a defect appears, change only one variable at a time. Document the result before making another adjustment. Changing media, compound, and machine settings simultaneously makes it impossible to identify the root cause.
- Extending cycle time arbitrarily. Longer is not always better. Extended cycles can cause edge rounding, heat buildup, and part-on-part damage without improving surface quality.
- Using the same process parameters for different materials. Aluminum, stainless steel, brass, zinc, and plastic each require different media, compound, and machine settings even for the same target finish.
- Neglecting regular media maintenance. Media wears down over time, losing its cutting edges and changing the process dynamics. Replace worn media according to the manufacturer guidelines.
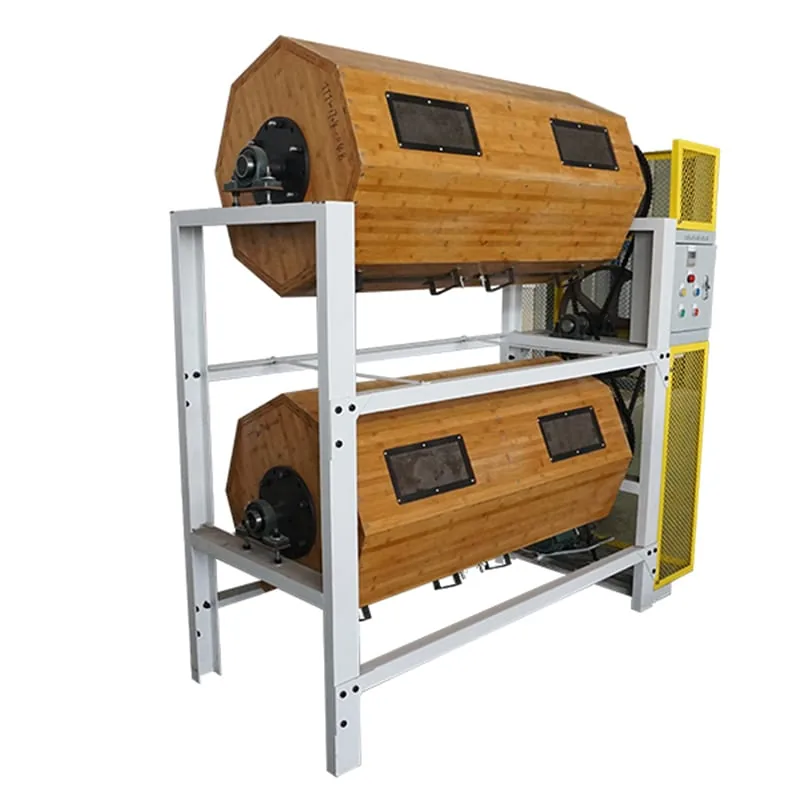
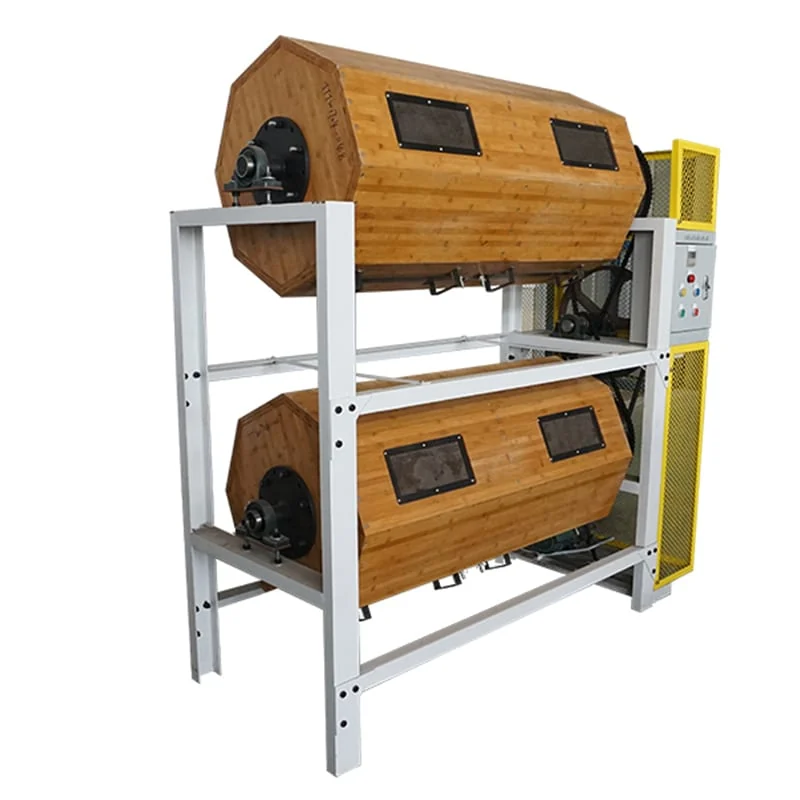
Visual Reference for Process Setup

See the Process in Action
Watch how surface finishing equipment processes parts in a real production environment:

Need to confirm a process before batch production? Send us your part material, photos, dimensions, current surface condition, and target finish. We can help review whether your issue is caused by media, machine settings, compound, water quality, or handling after finishing.
Related Solutions
These pages may help you compare suitable machines, media, compounds, and processes:
Need Expert Advice for Your Finishing Process?
Send us your part material, photos, dimensions, current surface condition, target finish, and batch quantity. Our team can help recommend suitable finishing machines, media, compounds, and a test process direction for your specific application.
| Part feature | Common risk | Starting direction | What to check |
|---|---|---|---|
| Very small holes and slots | Pins too large to enter the feature | Reduce pin size until it follows the geometry | Whether the feature is reached at all |
| Thin walls and fine edges | Edge rounding from prolonged action | Shorten the cycle before changing anything else | Edge condition against the starting part |
| Non-magnetic material | The process cannot act on the part | Confirm the material is magnetic before planning | Whether a different route is needed |
| Mixed part sizes in one batch | Small parts shield large ones | Run similar sizes together | Whether results differ part to part |
| Soft or plated surfaces | Surface marking or plating wear | Reduce cycle time and check the surface | Plating condition after processing |
Directions to test on a representative sample, not validated results for a specific component.
 +86-592-2381506


 IPv6 network supported
