PURCHASING SCOPE GUIDE How to Compare Mass Finishing Quotations for CNC Metal Parts Compare trial evidence, equipment scope, separation, drying and acceptance conditions before choosing a mass finishing quotation for industrial CNC parts. Quick answer: Two quotations with similar machine capacities may describe very different production systems. For CNC metal parts, compare the part specification ...
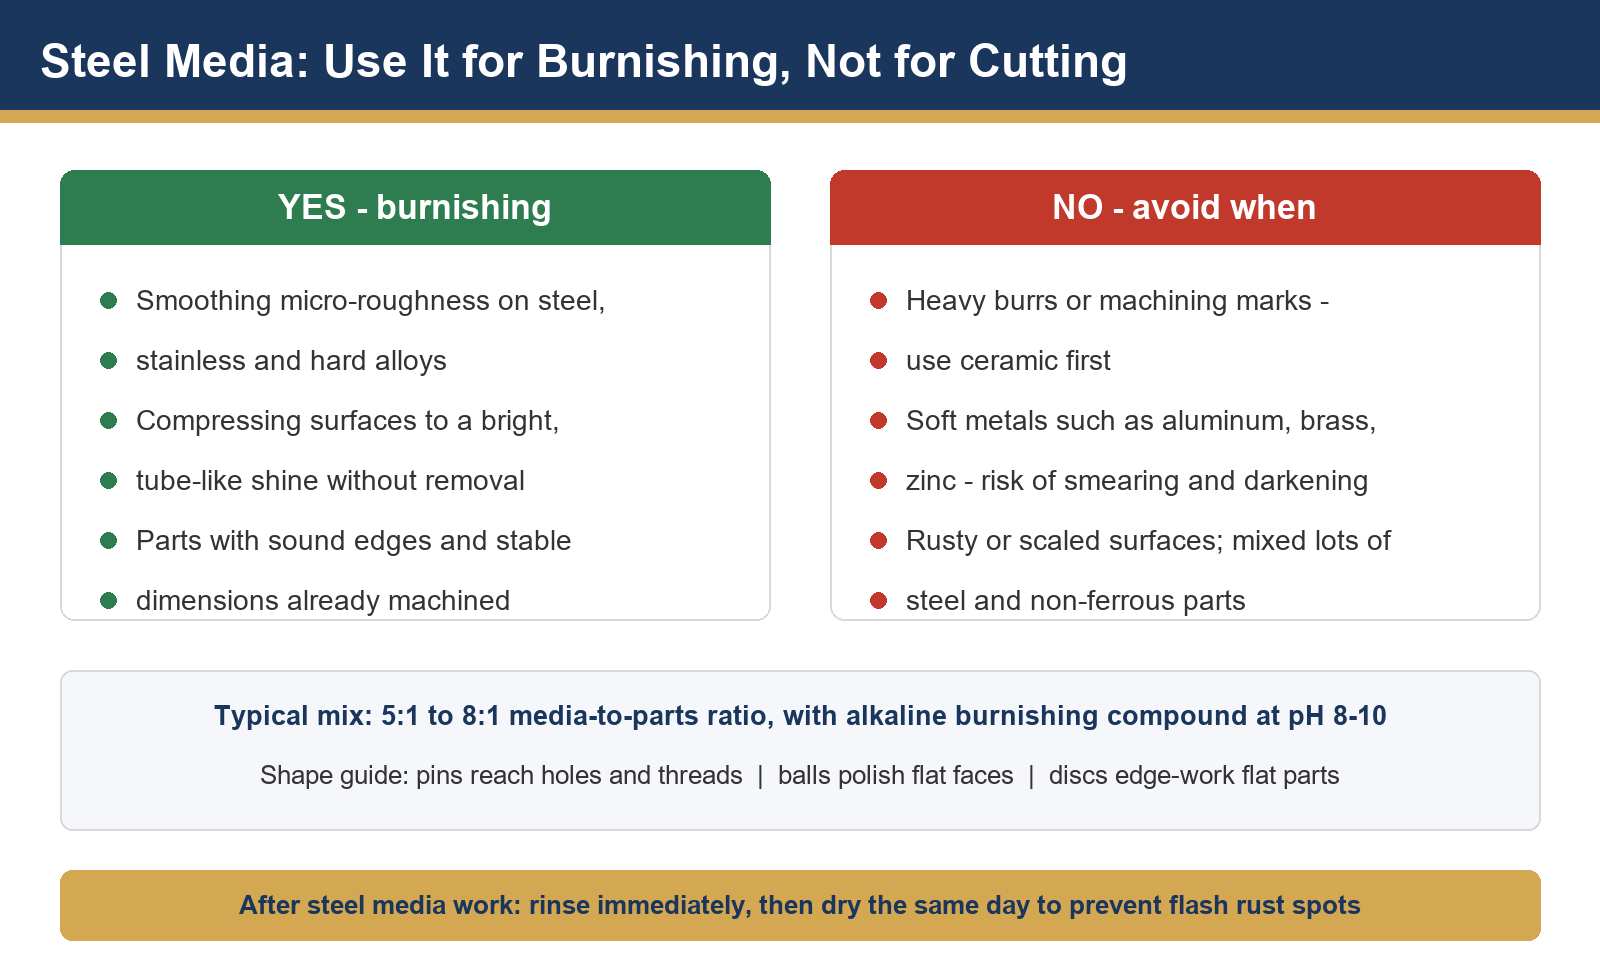
Steel Media Burnishing Guide: How It Creates Mirror Shine and When Not to Use It Steel finishing media • Pins, balls & discs • Burnishing process, compound pairing and limits Steel media is unique in mass finishing: it is the only media that polishes almost entirely without cutting. Hardened stainless pins, balls, and discs rub against parts under compound pressure, compressing micro-peaks int...
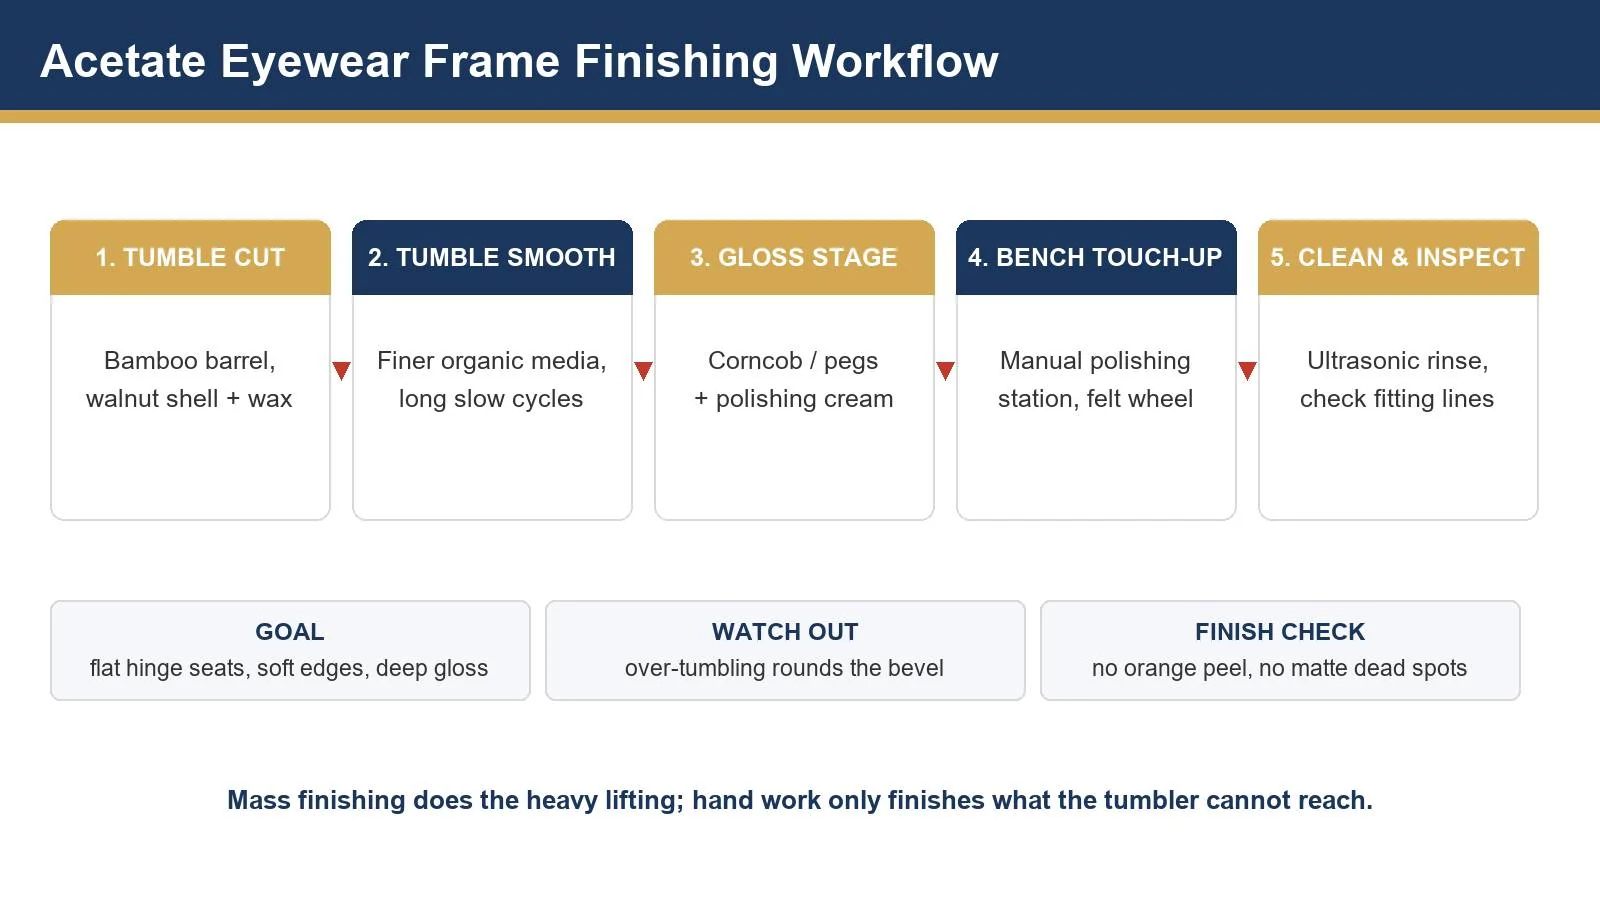
How Acetate Eyewear Frames Are Mass Finished: From Tumbled Matte to Mirror Gloss Acetate frame polishing workflow • Barrel tumbling + bench touch-up • A repeatable process for eyewear production Freshly milled acetate frames come off the CNC looking chalky, with tool marks along the bevels and matte hinge seats. Turning them into the deep, wet-look gloss that defines premium eyewear is a staged pr...
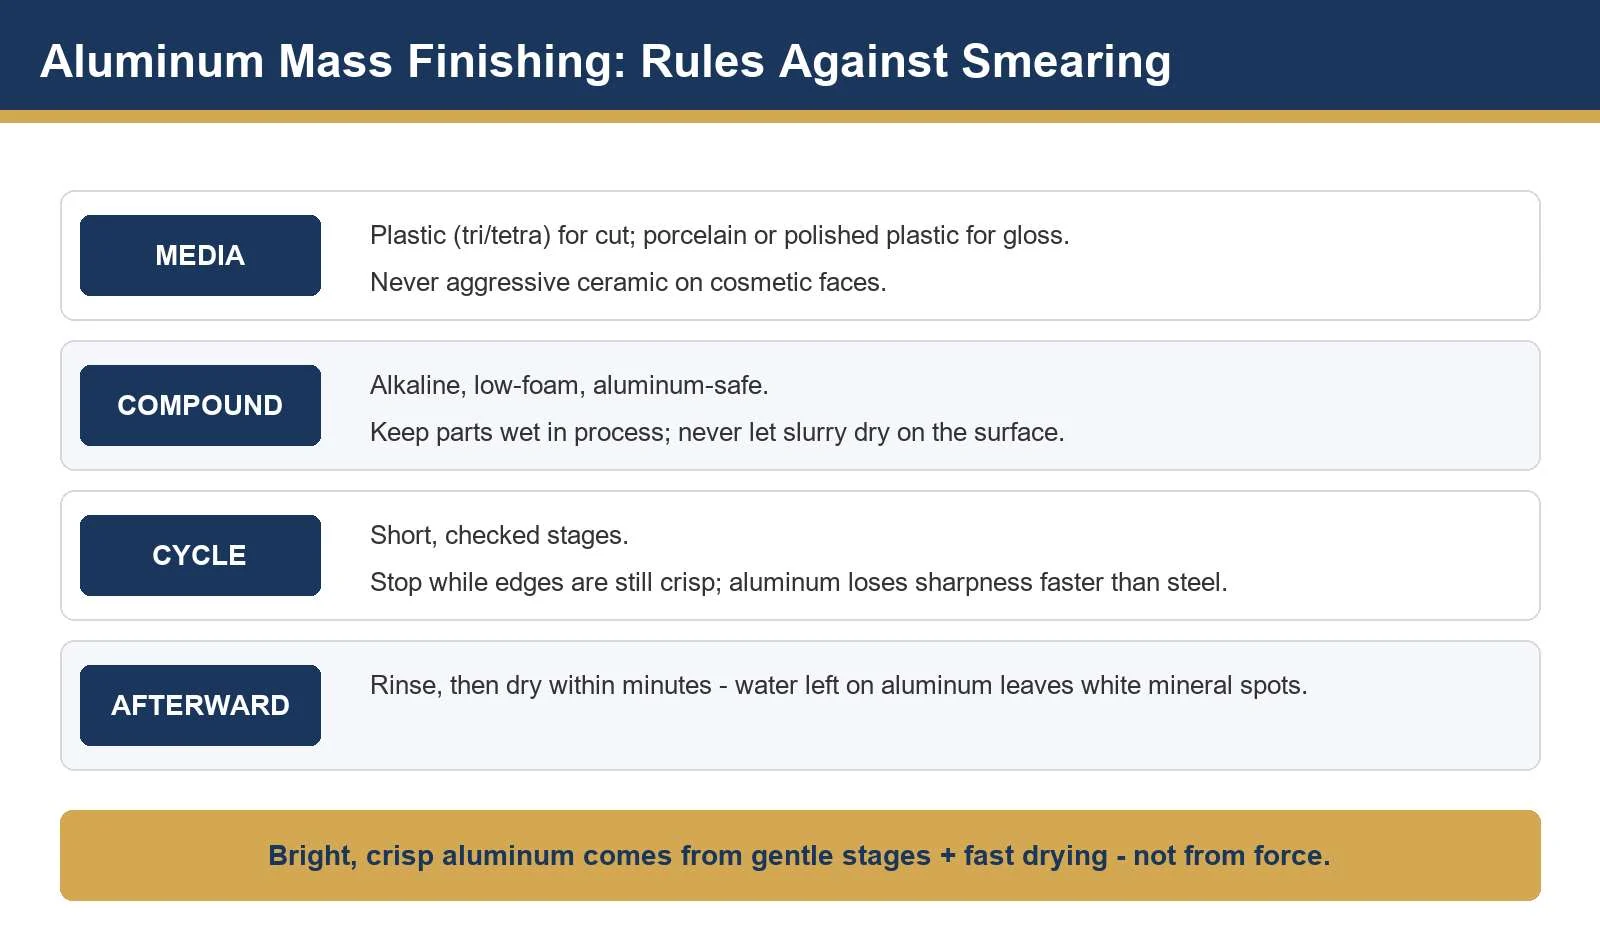
Mass Finishing Aluminum Parts: Deburr, Smooth and Brighten Without Smearing Aluminum surface finishing • Media, compound and cycle selection • From CNC parts to cosmetic components Aluminum is one of the most rewarding — and least forgiving — metals to mass finish. It deburrs fast, smooths beautifully, and polishes to an attractive satin-bright look. But it also smears under aggressive media, stai...
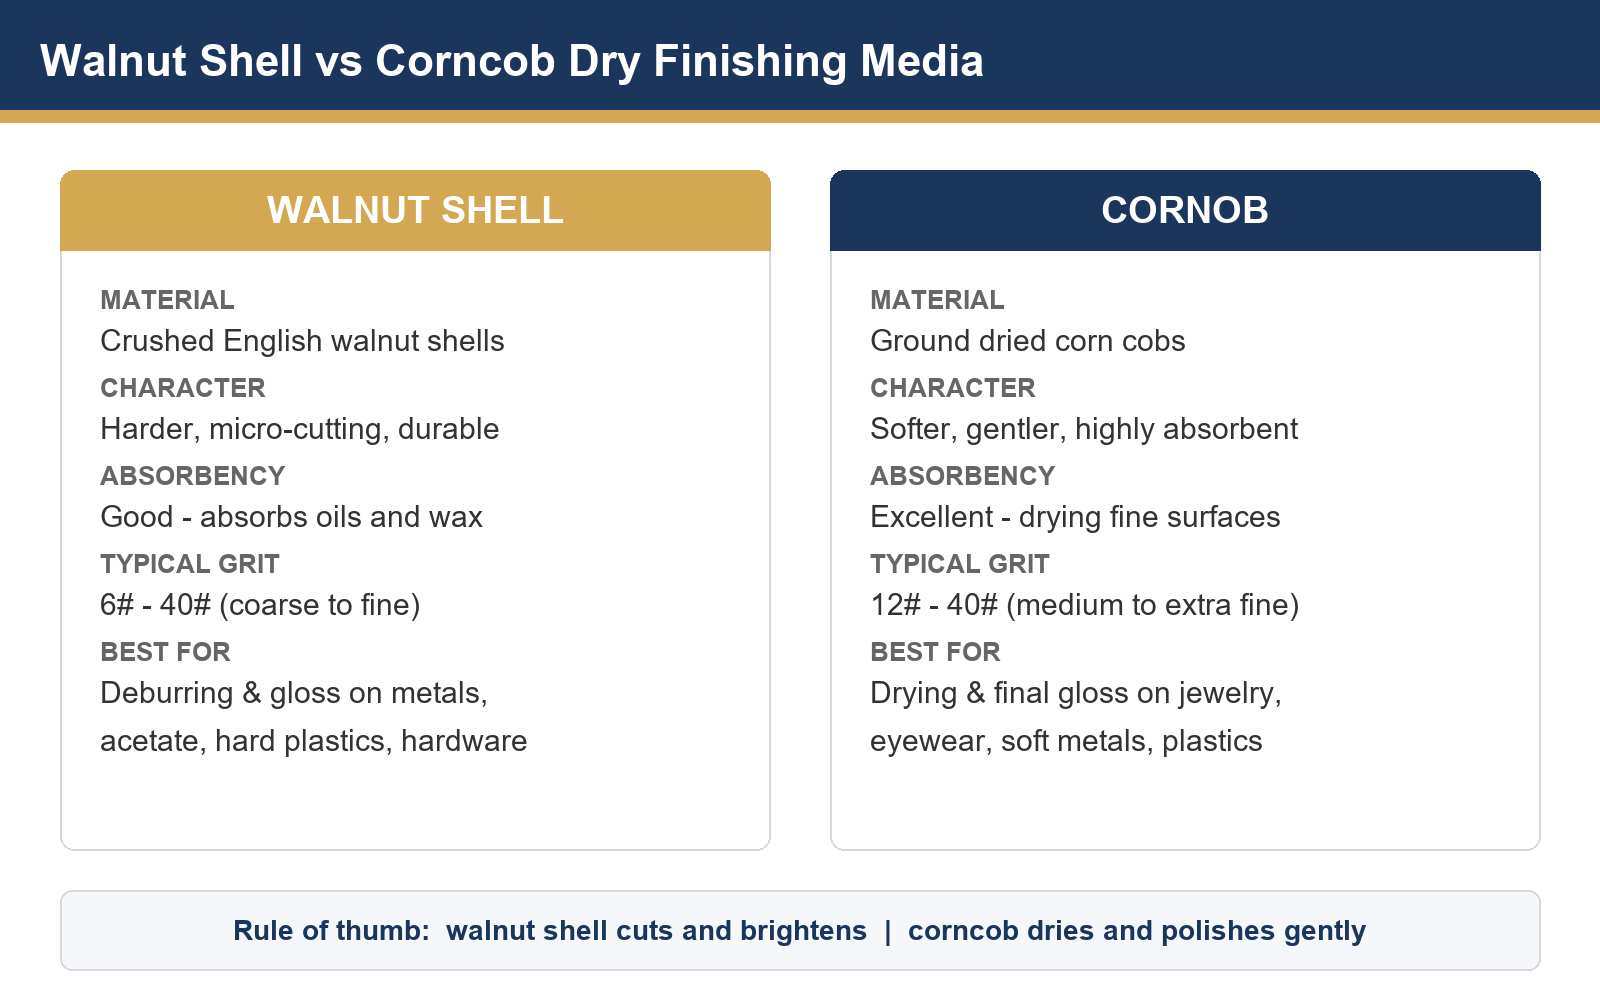
Walnut Shell vs Corncob: How to Choose Dry Tumbling Media for Eyewear, Jewelry & Hardware Dry finishing media selection guide • Walnut shell & corncob • For dry tumbling, vibratory and centrifugal lines Dry organic media — crushed walnut shell and ground corncob — is the workhorse of dry tumbling and dry vibratory finishing. The two materials look similar in the bag, but they behave very d...
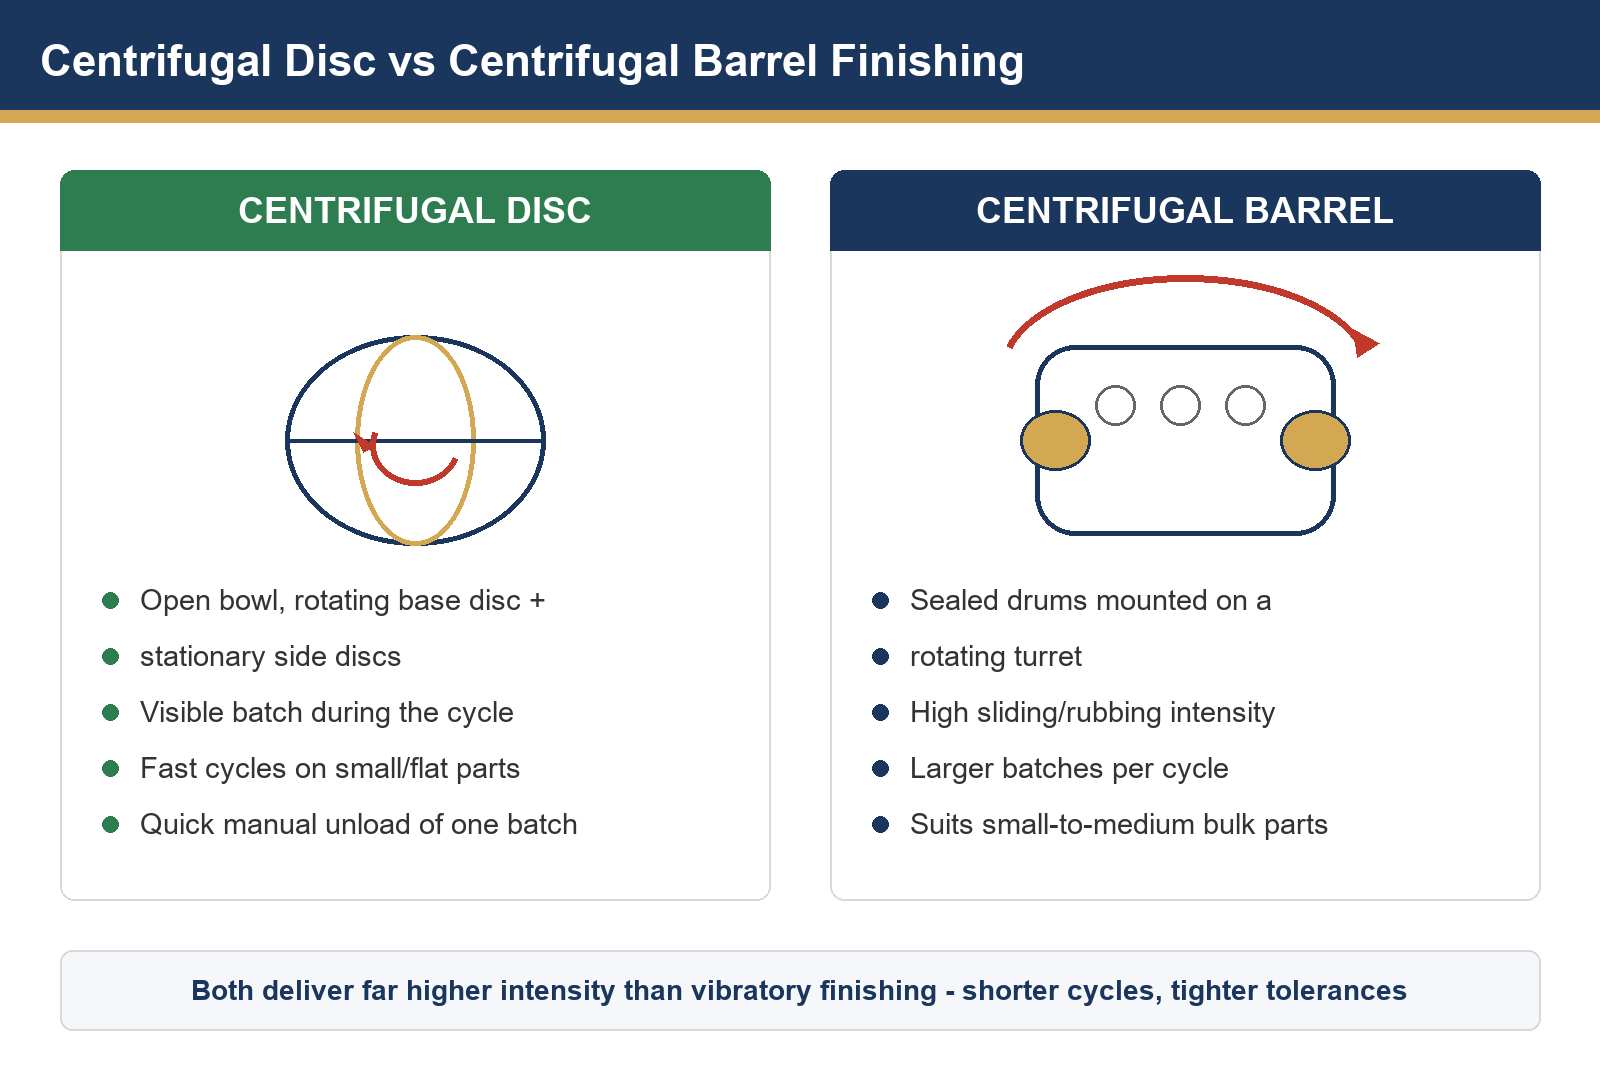
Centrifugal Disc vs Centrifugal Barrel Finishing: Which High-Energy Machine Fits Your Parts? High-energy mass finishing comparison • Centrifugal disc & centrifugal barrel • Machine selection guide When vibratory finishing is too slow or too gentle for the result you need, the next step up in intensity is a centrifugal disc or a centrifugal barrel machine. Both multiply the effective force betw...
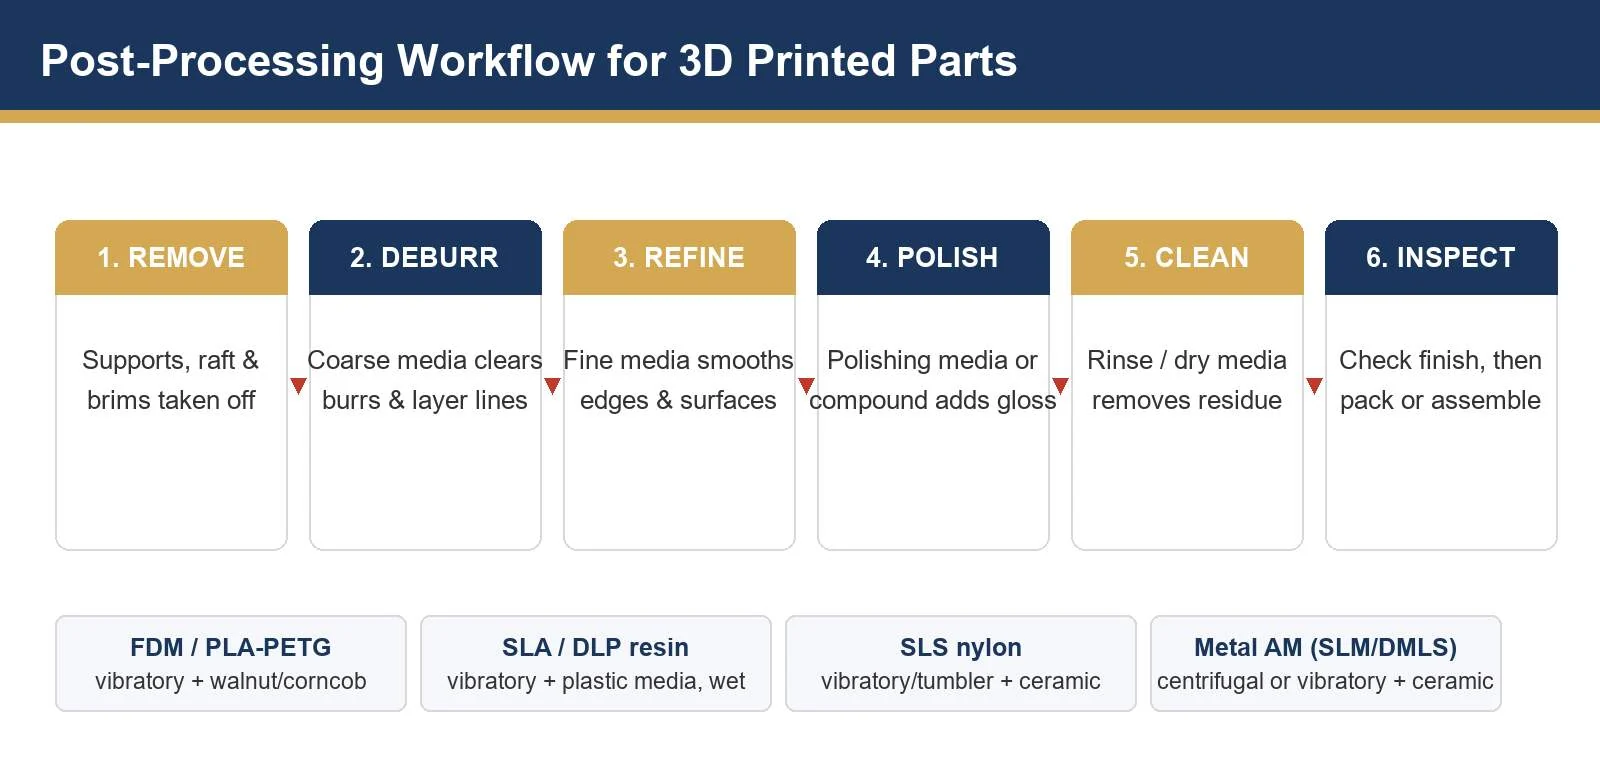
Mass Finishing for 3D Printed Parts: Deburring and Polishing Additive Manufacturing Components Additive manufacturing post-processing • Deburring, smoothing & polishing • FDM, SLA/DLP, SLS & metal AM parts 3D printing turns out parts close to final shape, but almost never close to final surface. Support scars, layer lines, partially fused powder, and sharp edges stand between a fresh print...
How to Choose Media Size for Small Holes, Slots and Internal Cavities How to Choose Media Size for Small Holes, Slots and Internal Cavities Short answer: choose the smallest media that reaches the required feature and can still be separated reliably. A smaller chip may improve access, but it can also lodge in a hole, pass through a slot, slow separation or change the contact intensity. The correct...
How to Prevent Part-on-Part Damage in Vibratory Finishing How to Prevent Part-on-Part Damage in Vibratory Finishing Short answer: part-on-part damage is usually a contact-control problem. Protect the workpieces with enough media coverage, a suitable media size and shape, a stable load ratio and a machine motion that keeps parts separated. Confirm the change with before-and-after inspection instead...
We use essential storage to keep this site working. With your permission, Google Analytics 4 helps us understand visits and improve the site. Advertising storage, ad user data, and ad personalization always stay off.



 IPv6 network supported


 +86-592-2381506
